


Why Do Changheng Plywood Cutting Blades Need the Right Design
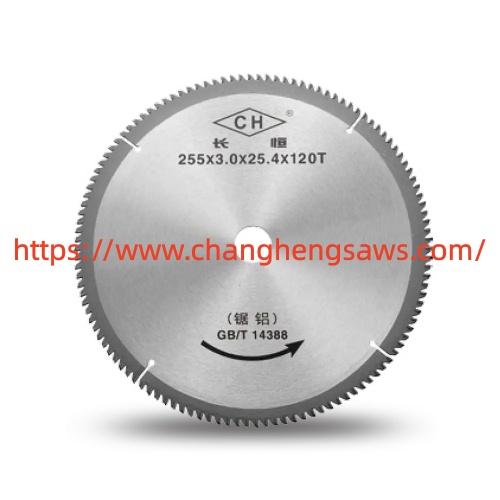
Plywood Cutting Blades play an important role in panel processing, where edge quality, dimensional accuracy, and production consistency can affect the final product. For furniture factories, cabinet makers, and woodworking equipment operators, selecting a suitable blade involves more than checking its diameter or tooth count. The material structure, surface finish, cutting direction, and machine configuration all influence how a blade performs during daily production. Changheng focuses on saw blade solutions for practical cutting applications, helping buyers consider the specifications that match their manufacturing requirements.
Plywood is made from layers of wood veneer bonded together, with adjacent layers usually arranged at different grain directions. This structure gives the panel useful strength, but it also creates challenges during machining. The cutting edge encounters changing grain orientations and adhesive layers, while the outer veneer may chip if the blade geometry or operating conditions are unsuitable. A blade intended for rough construction work may therefore produce a different finish from one selected for cabinet panels or decorative surfaces. Identifying the intended application should be the starting point for product selection.
Tooth geometry is one of the key features worth examining. Alternate top bevel, commonly known as ATB, uses teeth with alternating bevel directions to shear wood fibers during cutting. This design is often considered for crosscutting and applications where veneer damage needs to be controlled. Other tooth configurations may be appropriate for different materials or production methods. The choice depends on the panel surface, cutting direction, machine type, and finish requirements rather than a single specification applied to every job.
Tooth count also deserves careful consideration. A blade with fewer teeth generally provides more space for chip removal and can suit operations where cutting speed is important. A higher tooth count can produce a finer cut under suitable conditions, although the reduced space between teeth may increase heat or limit chip clearance when feed settings are inappropriate. For example, a workshop cutting structural panels for hidden applications may have different requirements from a factory producing visible cabinet edges. Selecting the tooth count according to the workpiece and process helps establish a practical balance between cutting speed and finish quality.
Kerf width is another specification that can influence production. Kerf refers to the width of material removed by the blade as it passes through a panel. A narrower kerf may reduce material loss and cutting resistance, particularly when used with compatible equipment. However, blade stability, panel thickness, feed pressure, and machine power must also be considered. A thin blade that does not match the equipment or cutting conditions may deflect, affecting the accuracy of the finished edge. Buyers should evaluate the complete cutting setup instead of treating kerf width as an isolated advantage.
Blade body construction and cutting edge material can affect service life and operating consistency. Carbide tipped teeth are widely used in woodworking because they can maintain a cutting edge through repeated processing when properly selected and maintained. The blade body also needs suitable flatness and stability for its intended operating speed. During purchasing, manufacturers should check the tooth material, body dimensions, arbor size, maximum rated speed, and application guidance. These details help reduce compatibility problems and support a more predictable maintenance schedule.
Machine conditions remain important even when the blade specification is appropriate. Incorrect alignment, worn bearings, excessive feed pressure, insufficient workpiece support, or resin deposits can contribute to rough edges and uneven cutting. Operators should inspect the equipment regularly, keep the blade clean, and follow the manufacturer's instructions for installation and maintenance. If chipping appears suddenly, checking the panel support and machine condition may be just as important as replacing the blade. Consistent inspection can help identify problems before they cause repeated rework or unnecessary material waste.
For buyers sourcing industrial saw blades, a clear understanding of the production task makes communication with a manufacturer more productive. Sharing the panel material, thickness, cutting direction, machine model, required finish, and expected operating conditions helps narrow the available specifications. Changheng can be considered as a manufacturing partner when evaluating blade options for different woodworking applications. To review available product information and identify a suitable solution for your processing needs, visit https://www.changhengsaws.com/product/ and compare the relevant specifications with your equipment and production requirements.
 Spanish
 English
 Arabic
 French
 Portuguese
 Deutsch
 Turkish
 Dutch
 Italiano
 Russian
 Romaian
 Portuguese (Brazil)
 Greek